Route report
The document that gets a part made.
A route report is what comes after the CAD: which process, on which machine, with which tool, how to tell it went right and what to buy. This is a real one, translated from the Spanish original: 10 phone cases in flexible polyurethane, cast in a mold printed on an Anet ET4.
- 10cases in the lot
- 25.98 cm³measured volume of one case
- 368 gresin with purge and losses
- ±0.7 mmacceptance on length and width
Nothing here has been cast yet. The report is the plan; the first article decides.
Why this route
A short lot and a part that can come out of the mold by flexing. The tooling is cheap and easy to change, the two halves fit on the printer, and the vents or the gate can move if the first article asks for it.
Process sheet
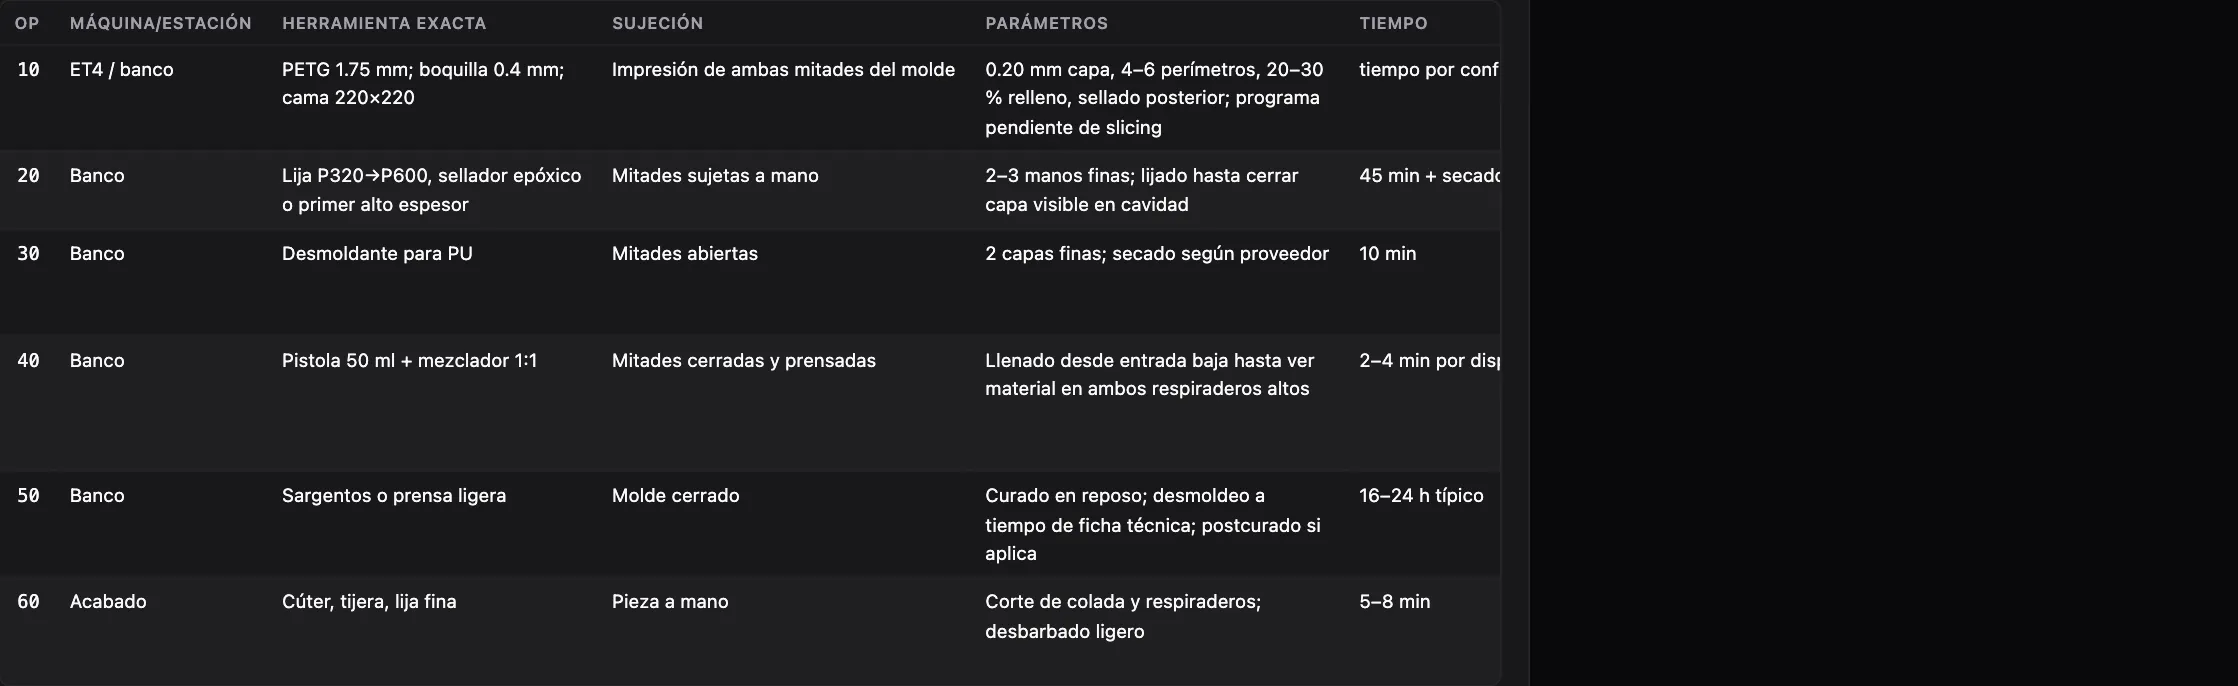
| Op | Station | Exact tool | Parameters | Time | What is checked | If it fails |
|---|---|---|---|---|---|---|
| 10 | Printer | PETG 1.75 mm, 0.4 mm nozzle | 0.20 mm layer, 4–6 perimeters, 20–30 % infill | To confirm | No warp over 0.5 mm, vents open | Reprint with a brim and a hotter bed |
| 20 | Bench | Sandpaper P320→P600, epoxy sealer or high-build primer | 2–3 thin coats, sand until the layer lines close in the cavity | 45 min + drying | Smooth cavity, no open pores | Seal and sand again |
| 30 | Bench | PU mold release | 2 thin coats, drying per supplier | 10 min | Continuous film, no puddles | Clean, reapply and let it dry fully |
| 40 | Bench | 50 ml dual-cartridge gun, 1:1 static mixer | Fill from the low gate until material shows at both high vents | 2–4 min per shot | Steady flow at the vents, no large bubbles; shot ±2 g | Purge, add a vent, or lower the viscosity |
| 50 | Bench | Light clamps | Cure at rest; demold per data sheet | 16–24 h typical | Not tacky; critical dimensions ±0.7 mm; fits without tearing | If soft or foamed: discard, dry the mold, check the mix |
| 60 | Finishing | Cutter, scissors, fine sandpaper | Cut gate and vents, light deburring | 5–8 min | Flash under 0.3 mm; camera window and port clear | If it tears: larger radius at the gate |
What is done and what is not
- DoneCAD: the case, 75.8 × 153.9 × 10.7 mm
Geometry saved
- DoneMold: printed halves, 4 keys, gate, 2 vents of 1.2 mm
Mold geometry check passed
- PendingSlicing for the printer
Not verified: the slicer was not installed on that computer
What it did not verify
Demolding force and tearing of the elastomer were not verified: only that the mold geometry passes and that the undercuts can come out by flexing. No G-code was generated, because the slicer was not installed on that computer.
Shopping list
| Item | Specification | Qty | Price (MXN) | Seller |
|---|---|---|---|---|
| Dual-cartridge gun | 50 ml cartridges, 1:1 / 1:2 | 1 | 452.98 | Amazon MX |
| Static mixer nozzles | Pack of 10, 1:1, 91 mm | 1 pack | 177.49 | Amazon MX |
| PETG filament 1.75 mm | 1 kg, both mold halves | 1 spool | 325.00 | Geek Factory |
| Scale | 500 g, 0.1 g resolution, tare | 1 | 159.00 | Steren |
| Premium mold release | Ease Release 200, 14 fl oz | 1 can | 736.00 | Amazon MX |
| Castable polyurethane | VytaFlex 60, 1:1 by volume; hardness to confirm | 1 kit | 747.16 | Amazon MX |
| Budget mold release | Spray, 20 ml | 1 bottle | 181.09 | Amazon MX |
| Mold sealer | Epoxy or high-build primer | 1 small kit | — | No verified offer |
Verified today: MXN 2,778.72, plus the sealer. Prices seen on 4-Nov-2026. Check them before buying.
First article: how it is accepted
- Complete fill, with no open bubbles at the corners or in the camera window.
- Length and width with calipers, within ±0.7 mm of the saved CAD.
- Fit on the real phone or a dimensional dummy: goes on with moderate effort and stays on when held upside down for 10 s.
- USB-C port clear and camera window off the lenses.
- Weigh it and use that as the reference: reject parts off by more than ±10 %.
Risks and protection
- Isocyanates and PU vapours: nitrile gloves, goggles, cross ventilation, and a respirator if the supplier asks for one.
- Cutter and deburring: cut away from the hand, with the part supported.
- Printing: stay off the hot nozzle and bed, and watch the first layers.
- Waste: let leftovers cure before disposal; nothing down the drain.
The original, as Patok Lab wrote it